
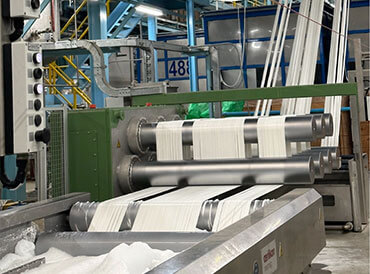
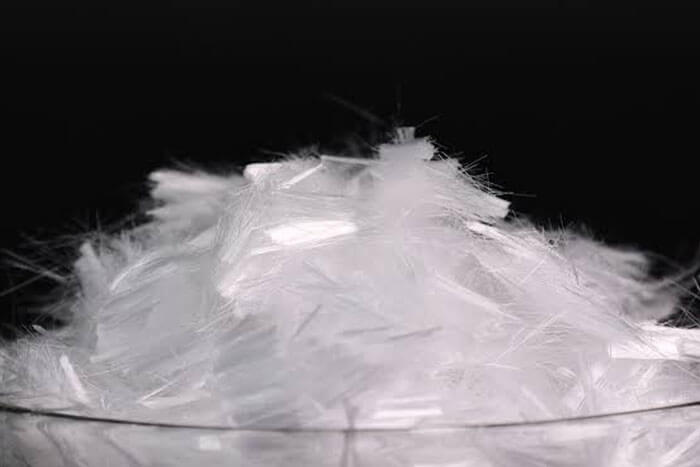
High-quality chemical raw materials, stable supply, meeting diverse industrial production needs.
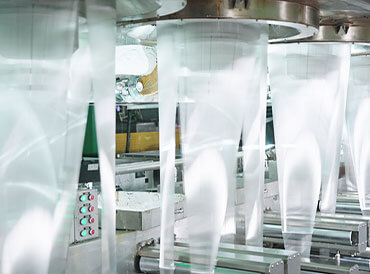
Professional R&D team providing customized technical solutions and process optimization.
Full-process safety control, efficient delivery, ensuring goods arrive safely and on time.
24/7 professional technical consulting to safeguard your production and operations.

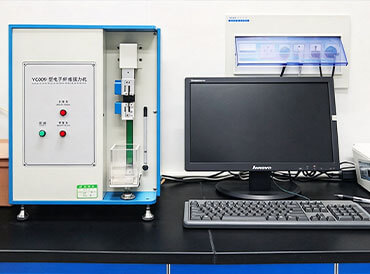
Rigorous quality control ensures purity and stability for every batch of raw materials.

Bespoke testing protocols for accurate, reliable data.
To be a trusted partner in the global chemical industry, delivering innovative and sustainable solutions.
Integrity, safety, and customer-first — the foundation of everything we do.
Market-oriented, customer-centered, and committed to continuous innovation.
To create sustainable value for customers, employees, and shareholders alike.
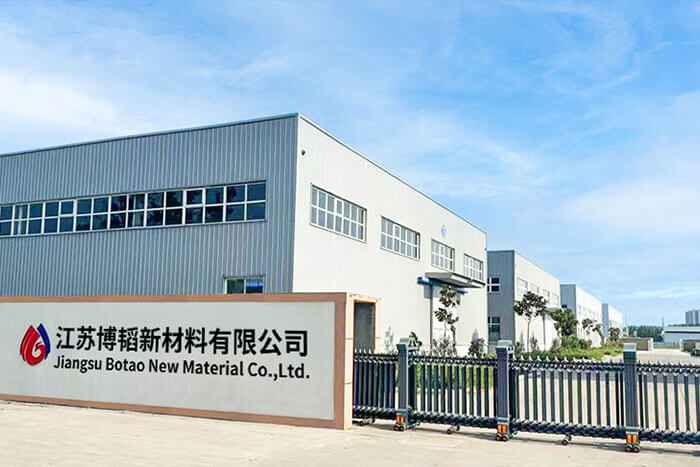
We are dedicated to sustainable practices that protect our planet while delivering value to our customers and communities.
Our factory has implemented cutting-edge manufacturing technologies that reduce environmental footprint while maintaining superior product quality. This initiative demonstrates our commitment to sustainable production practices in the chemical manufacturing sector. Recent upgrades to our production facilities have resulted in significant energy savings, reducing carbon emissions by optimizing reaction conditions and implementing advanced heat recovery systems. The new water recycling infrastructure allows for 95% reuse of process water, minimizing freshwater consumption and reducing wastewater discharge. This system sets new standards for water stewardship in chemical manufacturing operations.
Our R&D scientists have developed a proprietary catalyst formulation that significantly improves product yield and purity in organic synthesis processes. This innovation represents a major advancement in fine chemical manufacturing capabilities. Partnership with leading academic institutions has accelerated development timelines for next-generation manufacturing technologies. This collaborative approach combines theoretical research with practical industrial applications. Our quality assurance team showcased advanced analytical methodologies that enable real-time monitoring of critical process parameters, ensuring consistent product specifications batch after batch.
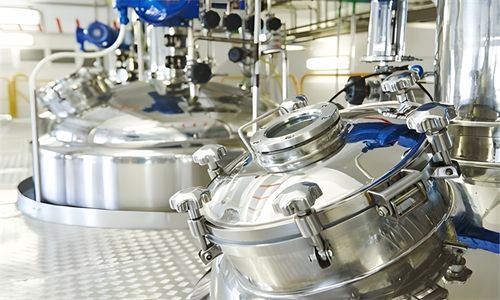
Our dedicated manufacturing line for custom specialty chemicals has received industry recognition for exceptional quality control and product consistency. This achievement reflects our expertise as a premium supplier to diverse industrial sectors. Implementation of state-of-the-art automation technology has significantly improved production precision and reduced variability. This system ensures exacting specifications are met for every order, regardless of volume. Working closely with strategic partners, our technical team developed a specialized chemical formulation that outperforms industry benchmarks. This success demonstrates our capability to create tailored solutions that address specific application challenges.
Dedicated to excellence in chemistry — serving industries worldwide with integrity and innovation.


